Complex Profiles and Special Geometries
Forms that have to carry abrasive into a narrow rib, an internal radius, a sharp shoulder or a stepped section — shapes a plated coating can follow and a pressed wheel cannot easily reproduce.
Grinding Wheel Products
Electroplated diamond tools hold a single layer of diamond in a plated metal coating applied directly to a precision-formed body. The coating follows the body, so the tool can carry fine detail, thin sections and complex profiles that would be difficult to produce any other way — and the exposed grain gives a free, open cut on hard materials.
Product Gallery
Discs, cones and profile forms
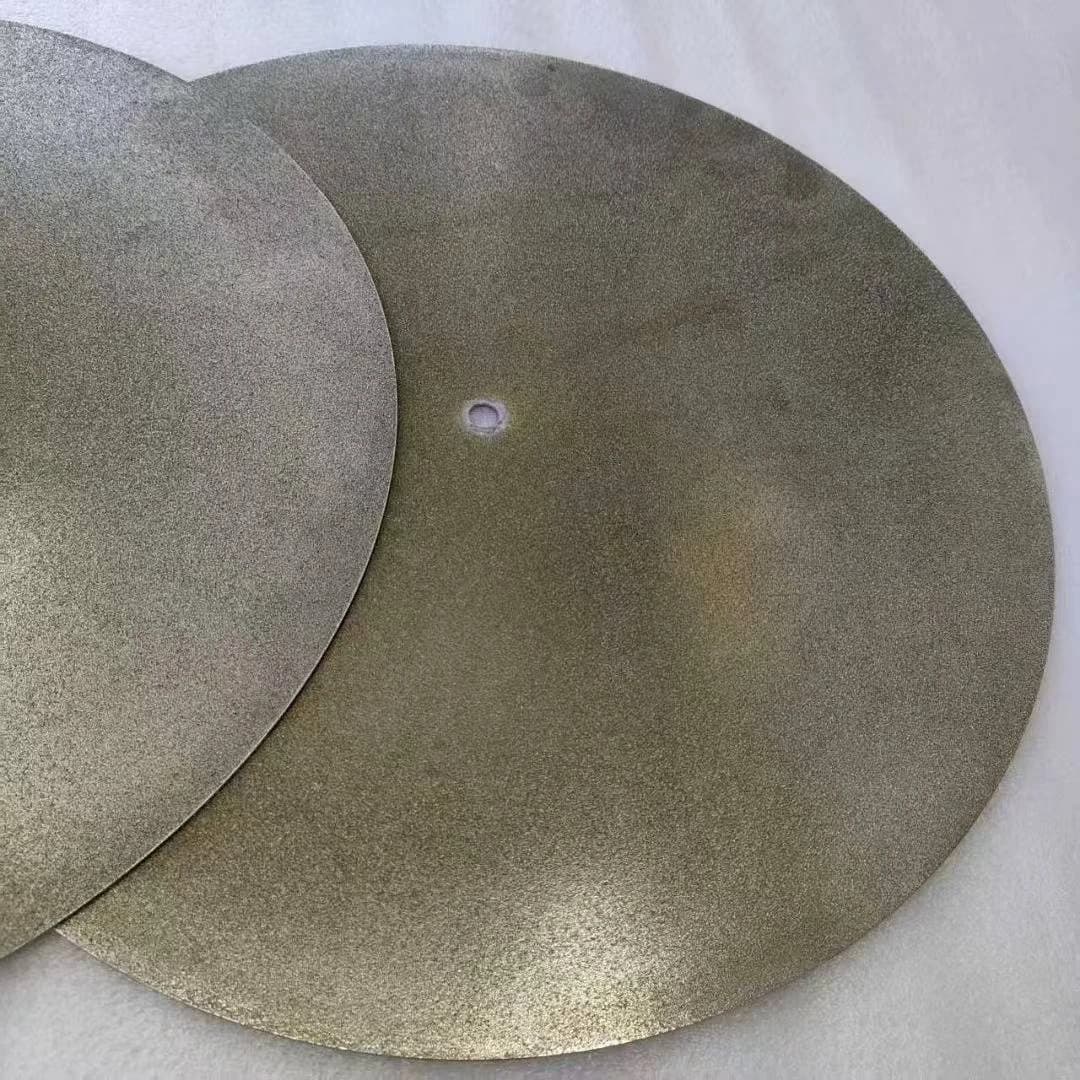
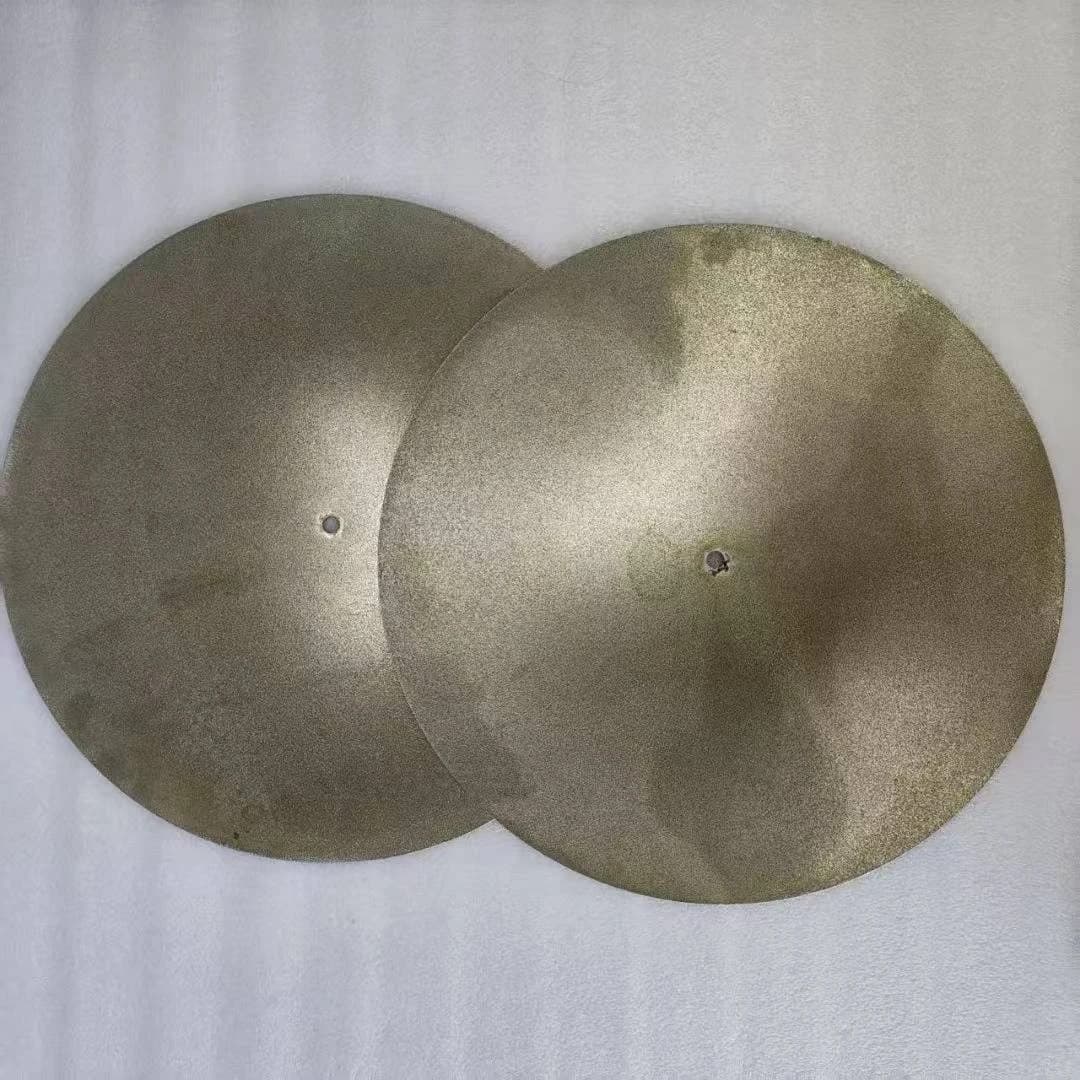
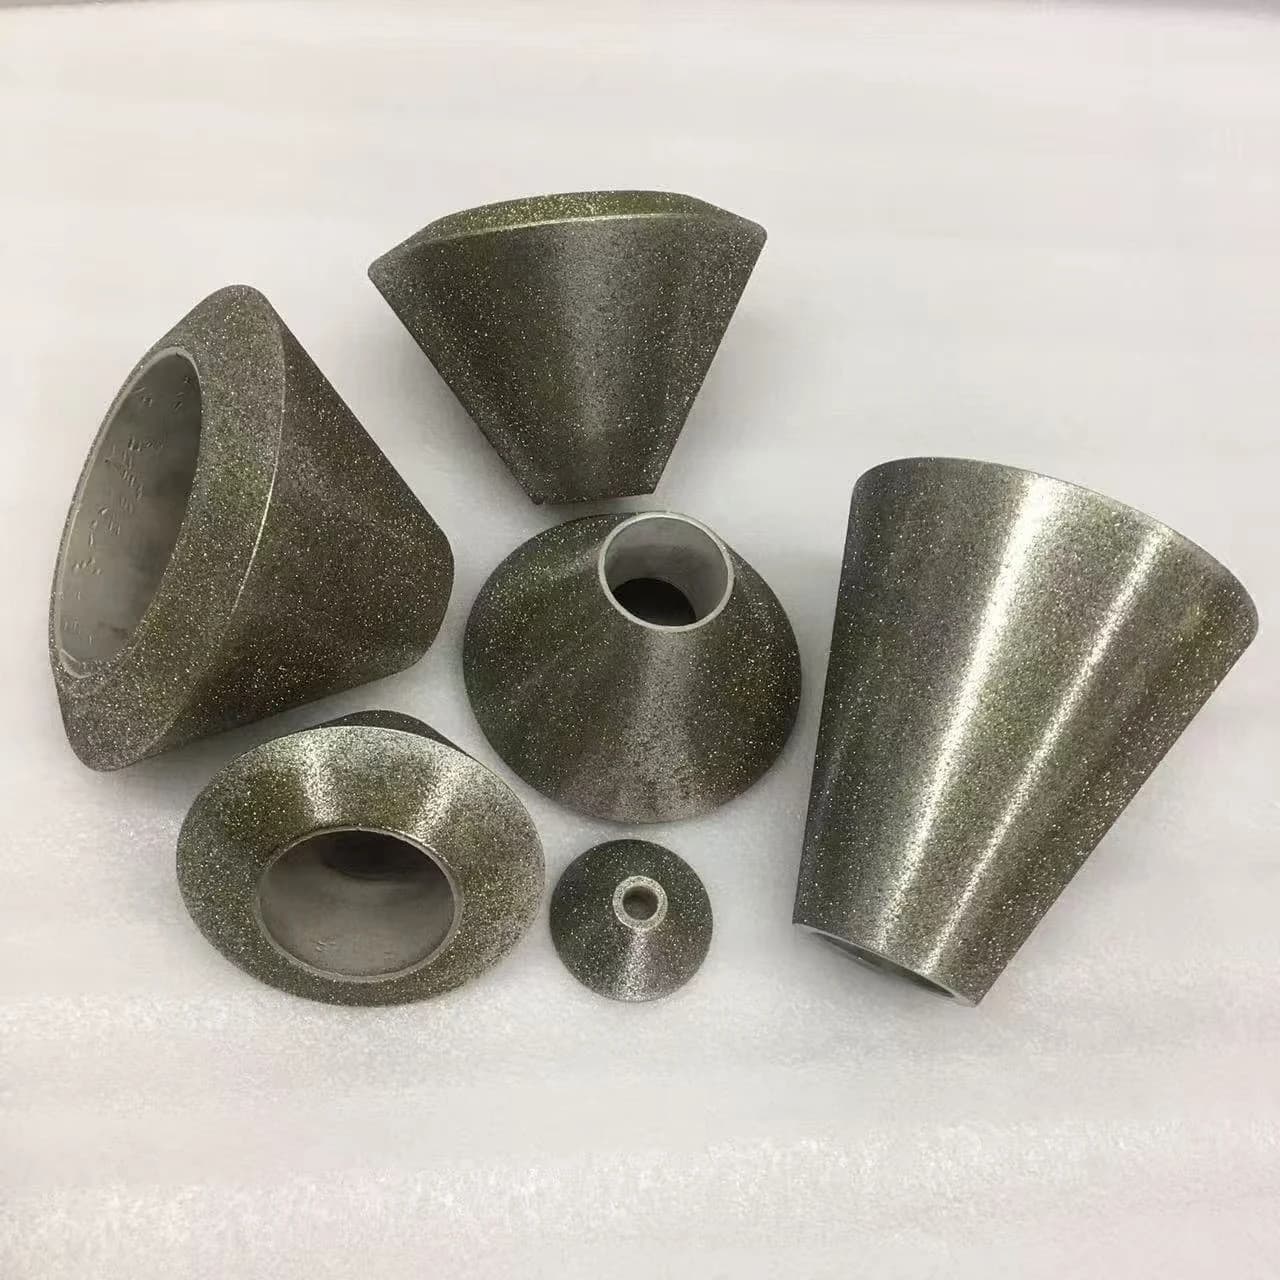
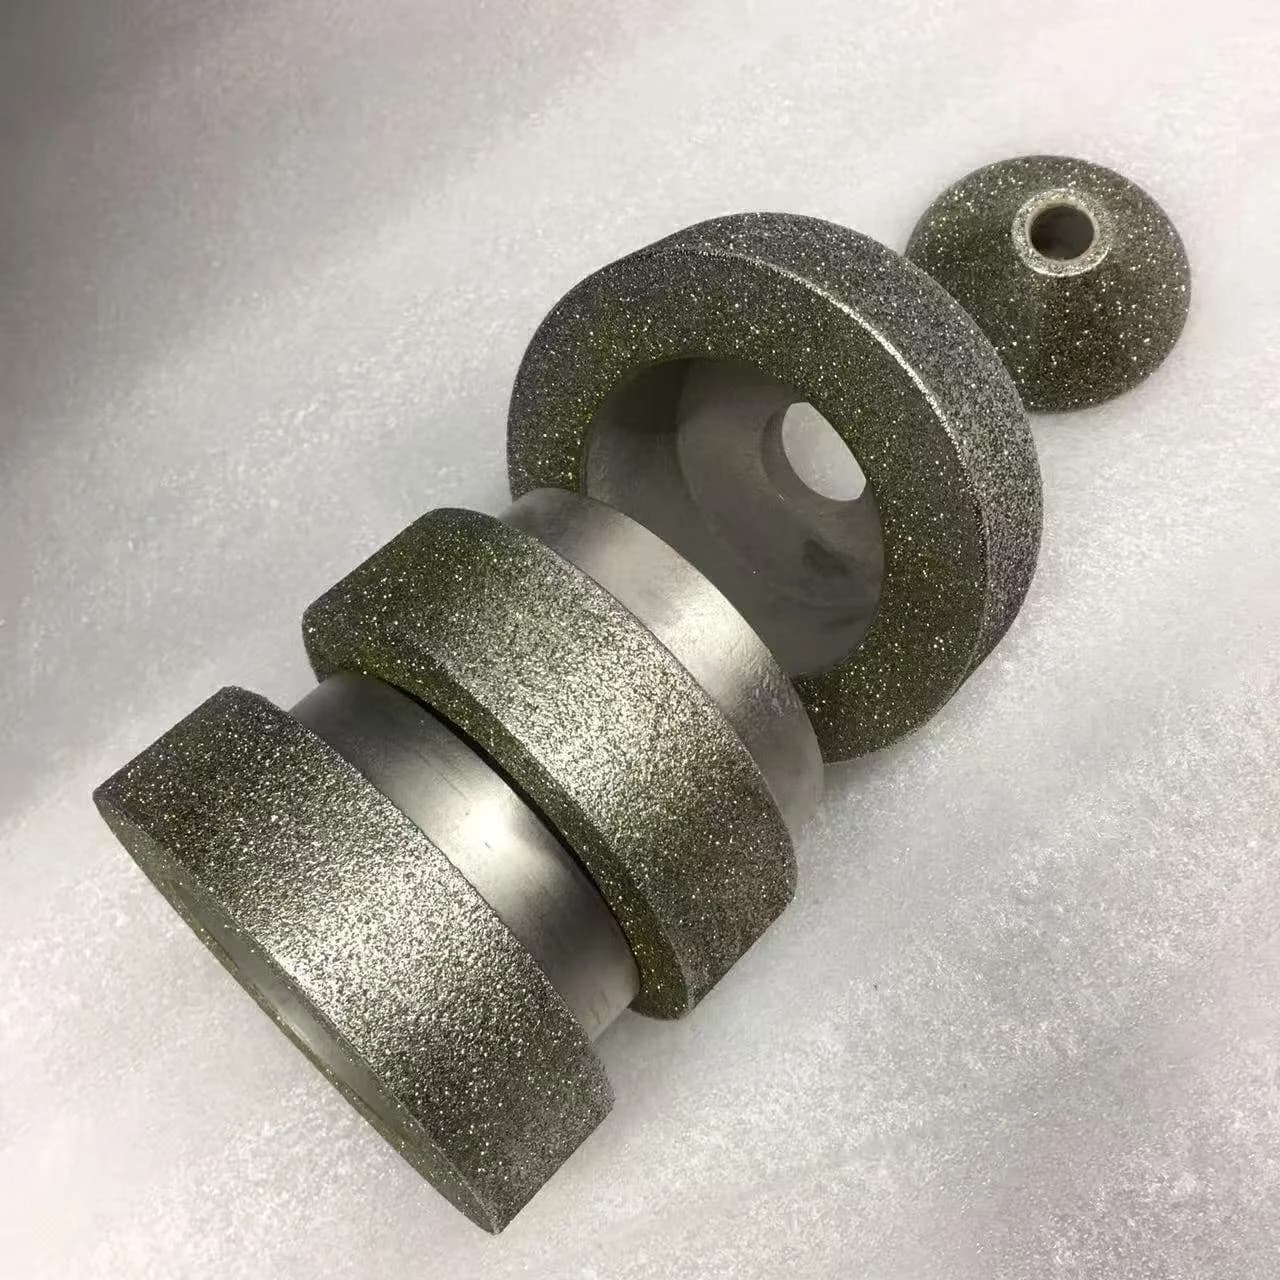
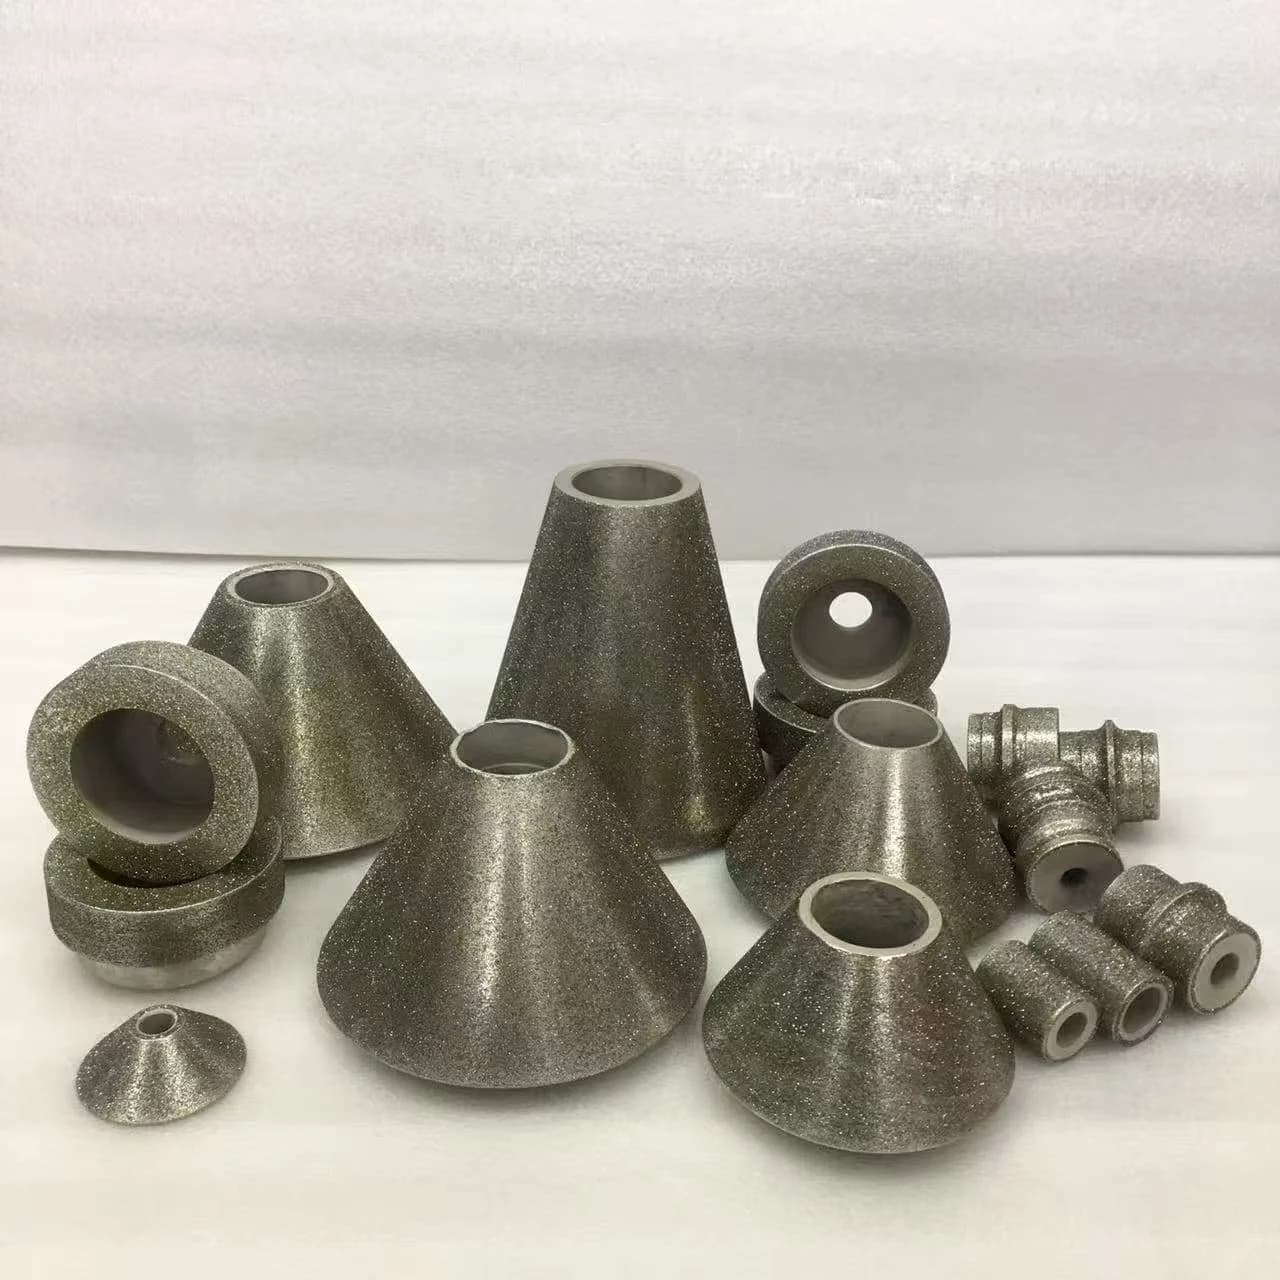
Electroplated diamond tools in disc, cone and profile forms. The coating follows the body geometry, so special shapes can be produced to a drawing.
Overview
Electroplated diamond tools are made by plating a metal coating, with diamond grain held in it, directly onto a body that has already been formed to the required shape. Because the coating is deposited rather than pressed, it follows the body geometry closely: narrow ribs, fine radii, sharp shoulders, thin walls, cones and small-diameter forms can all carry abrasive where it is needed.
The single layer of diamond sits proud of the coating, so the tool cuts with a high, open grain protrusion. That leaves room around each grain for chips and coolant, which is why these tools are used on hard materials where a closed or loaded face would rub rather than cut. As with any single-layer tool, the working life is set by that layer, so the specification is chosen around the material, the geometry and the operation.
Applications
Electroplated Diamond Tools are selected for these industrial grinding applications.
Forms that have to carry abrasive into a narrow rib, an internal radius, a sharp shoulder or a stepped section — shapes a plated coating can follow and a pressed wheel cannot easily reproduce.
Thin discs, shaped sections and small-diameter tools where the body is formed first and the abrasive is then applied to it.
Cemented carbide and tungsten carbide work, where diamond is the abrasive that cuts the material and an open face helps clear the fine swarf.
Hard brittle materials where diamond grain and a free-cutting face reduce heat and edge damage compared with a rubbing action.
Materials that are abrasive to the tool and hard to cut cleanly, where diamond grain is the appropriate abrasive direction.
Small-diameter tools, mandrel-mounted forms and one-off geometries produced to a drawing where no standard tool exists.
Workpiece Materials
Below are the most common workpiece materials matched with these grinding wheel applications.
A core application for diamond abrasive, including forms where the tool geometry does the shaping.
Technical and industrial ceramics, ground with diamond because conventional abrasive wears too quickly on them.
Glass shaping, edging and detail work, where the tool form and the diamond grain both affect the result.
Hard mineral materials where diamond abrasives are the established direction.
Abrasive, difficult-to-cut materials where an open diamond face is appropriate.
Diamond is not used on ordinary carbon steel because it reacts with iron at grinding temperature. Hardened ferrous work is ground with CBN, and soft steels with conventional abrasive. The workpiece material is confirmed before a tool is proposed.
Advantages
Electroplated diamond tool selection depends on the workpiece material, its hardness, the stock to be removed, the finish required, the machine, the operating speed, the coolant, the contact area and the tool geometry. Because those conditions differ between plants — and often between two machines in the same plant — Youlin Abrasive works from the actual grinding conditions rather than from a fixed catalogue of standard tools.
Diamond suits hard brittle non-ferrous materials — carbide, ceramics, glass, stone and composites. It is not used on ordinary carbon steel. Material is the first question in the review, not the last.
Electroplating is chosen when the shape is the difficult part: narrow ribs, fine radii, thin sections and small forms. That makes the drawing, not only the abrasive, the core of the specification.
Tool diameter, running speed and what the spindle can carry all limit what can be made, and thin or small tools are constrained in ways a standard wheel is not.
An open plated face helps, but how the coolant reaches the contact area still determines how much heat the diamond and the workpiece see.
A tool set up for removal and one set up for a controlled finish are specified differently, even when the geometry is the same.
The abrasive is a single plated layer, so the tool works until that layer is spent. The specification is chosen around the material and the geometry rather than for maximum life at any cost.
Customization
Each of the following is made to order and selected according to the application and the grinding conditions, rather than supplied as a fixed standard.
Tool diameter — selected according to the machine, the spindle and the working speed the operation runs at.
Width, thickness and section — set by the geometry required, the contact area and the stock to be removed.
Bore and mounting — matched to the spindle, arbor or mandrel the tool runs on, and to the mounting method you use.
Tool profile — cones, tapers, rings, thin discs, radii, ribs and stepped forms are produced to the required geometry.
Abrasive specification and grit size — selected according to the workpiece material and the surface, edge or detail quality required.
Coating and body material — reviewed together with the operation, since the plated coating holds the grain and the body carries the form.
Diamond layer where applicable — reviewed with the application rather than fixed in advance.
Application-specific geometry — small forms, thin walls, sharp shoulders and non-standard shapes can be produced to a drawing.
Before You Inquire
With plated tools the geometry usually drives the specification, so a drawing of the required form is the most useful starting point.
Send these details through the inquiry form, or contact us on WhatsApp. For small or non-standard forms, a drawing with tolerances lets us confirm what can be produced.
Send Grinding Details →Industries
Electroplated Diamond Tools are used across these manufacturing sectors. We provide grinding wheel solutions for industrial grinding applications. We do not supply the customer workpieces themselves, such as bearings, hydraulic components, molds, or mechanical parts.
FAQ
Quick answers to common buyer questions before sending an inquiry.
They are used where a single layer of diamond has to follow a specific shape — complex profiles, thin sections, small forms, cones and detail work — on hard, brittle non-ferrous materials such as cemented carbide, ceramics, glass, stone and composites. They are not used for ordinary carbon steel grinding.
Both carry a single layer of diamond on a formed body, and both give an open, free-cutting face. The difference is how the grain is held: electroplating deposits a metal coating with the diamond in it, which suits fine detail, thin sections and complex geometry, while brazing fixes the grain with a brazed coating that generally gives a stronger individual grain bond and a higher protrusion for heavier work. Which one suits an application depends on the material, the geometry and the load on the tool.
Yes. The body is formed first and the abrasive is applied to it, so the tool can be made to a specific geometry. Send the drawing with dimensions and tolerances, the material being ground, and the machine the tool runs on, and we will confirm what can be produced and propose a specification.
Only the abrasive tools. Youlin Abrasive is a grinding wheel and abrasive tool manufacturer. We supply the electroplated diamond tools used on carbide, ceramic, glass, stone and composite workpieces. We do not manufacture or supply the workpieces, the machine tooling, or the parts being ground.
Workpiece material and grade, the operation, tool dimensions, the required profile with a drawing where the shape matters, machine model and spindle speed, how the tool is mounted, coolant type and delivery, and the finish, edge or tolerance target. A photo or sample of the tool in use now helps us match the form.
Explore More
Continue browsing related products, applications, and technical information.