Grinding Wheels for Hydraulic Pump Valve Plates: Selection, Flatness & Surface Finish

Grinding Wheel Knowledge Base

Grinding Wheels for Hydraulic Pump Valve Plates: Selection, Flatness & Surface Finish

A valve plate that is smooth but not flat will still leak. That single sentence explains most of the confusion around valve plate grinding: the face has to satisfy two different requirements at once, and one of them cannot be fixed by choosing a finer wheel. This guide shows which wheel families to evaluate for the plate material in front of you, which workpiece details decide the answer, and what to send before anyone can recommend a specification.

Flatness and surface roughness are separate requirements with separate causes
Steel, cast iron, bronze and multi-material plates do not share one wheel
A finer grit cannot correct a flatness deviation caused by heat or workholding
The drawing, the fixture and the current failure mode decide more than the wheel name

Overview

Quick answer

There is no single grinding wheel specification for hydraulic valve plates. The face grinding wheel has to be selected against four things: the plate material and its condition, the flatness and roughness requirements on the drawing and how they are measured, the machine and workholding that hold the plate, and the failure mode currently being seen — burn, loading, poor finish, flatness drift or short dressing life.

For many cast iron and general steel plates, a conventional aluminium oxide or silicon carbide wheel in a suitable bond is the first family to evaluate. Hardened ferrous plates in stable, higher-volume production are the usual case for evaluating CBN. Diamond is a separate discussion: it is not a general-purpose choice for ferrous valve plates, because diamond reacts with iron at grinding temperature. Bronze and other non-ferrous plates need their own review, since the wheel has to stay open in a soft, gummy material.

The usable output of this page is a complete application record. Send the plate drawing, material and condition, the flatness and roughness requirement with its measurement method, the fixture, the wheel currently used and the defect being produced. That is what makes a wheel recommendation possible instead of a guess.

Youlin supplies grinding wheels and abrasive tools only. Valve plates are customer workpieces. Final suitability may require technical review, a sample confirmation or a controlled trial on the customer's machine.

Start with the face, not the wheel

  • Write flatness and surface roughness as two separate acceptance requirements on the inquiry.
  • Identify the plate material and whether the ground face is base metal, a hardened layer or a coating.
  • Record where the flatness deviation appears — centre, edge, across ports — before changing the wheel.
  • A finer grit changes texture. It does not correct a face that is out of flat.
  • Match the wheel family to the material first, then refine grit, grade, bond and structure.

Why Valve Plate Face Grinding Matters

A valve plate is a sealing and running surface. The ground face has to do two jobs: hold the running clearance and stay flat enough to seal while the rotating group passes over it.

The face is a sealing surface, not a decorative finish

Surface texture and form both influence how the plate seals and wears. A face that measures smooth can still leak if the geometry is not flat, and a face that is flat can still wear quickly if the texture is wrong for the application. Neither result can be judged by eye or by touch.

Grinding sets the geometry after heat treatment and machining

Face grinding is usually the operation that establishes the final face condition. That means it inherits distortion from earlier operations and hardening, and it is also where any residual distortion becomes visible. Reviewing the upstream condition is part of the wheel review, not separate from it.

The plate is often thin relative to its face

Thin plates deflect under clamping and magnetic holding, and they move as heat builds. A wheel that cuts freely and a fixture that does not impose its own distortion are both part of getting a flat result.

The failure shows up downstream

A marginal face may still assemble and pass a short test, then show leakage, noise, pressure loss or wear in service. That is why the acceptance requirement has to come from the component's function, not from what the previous wheel happened to produce.

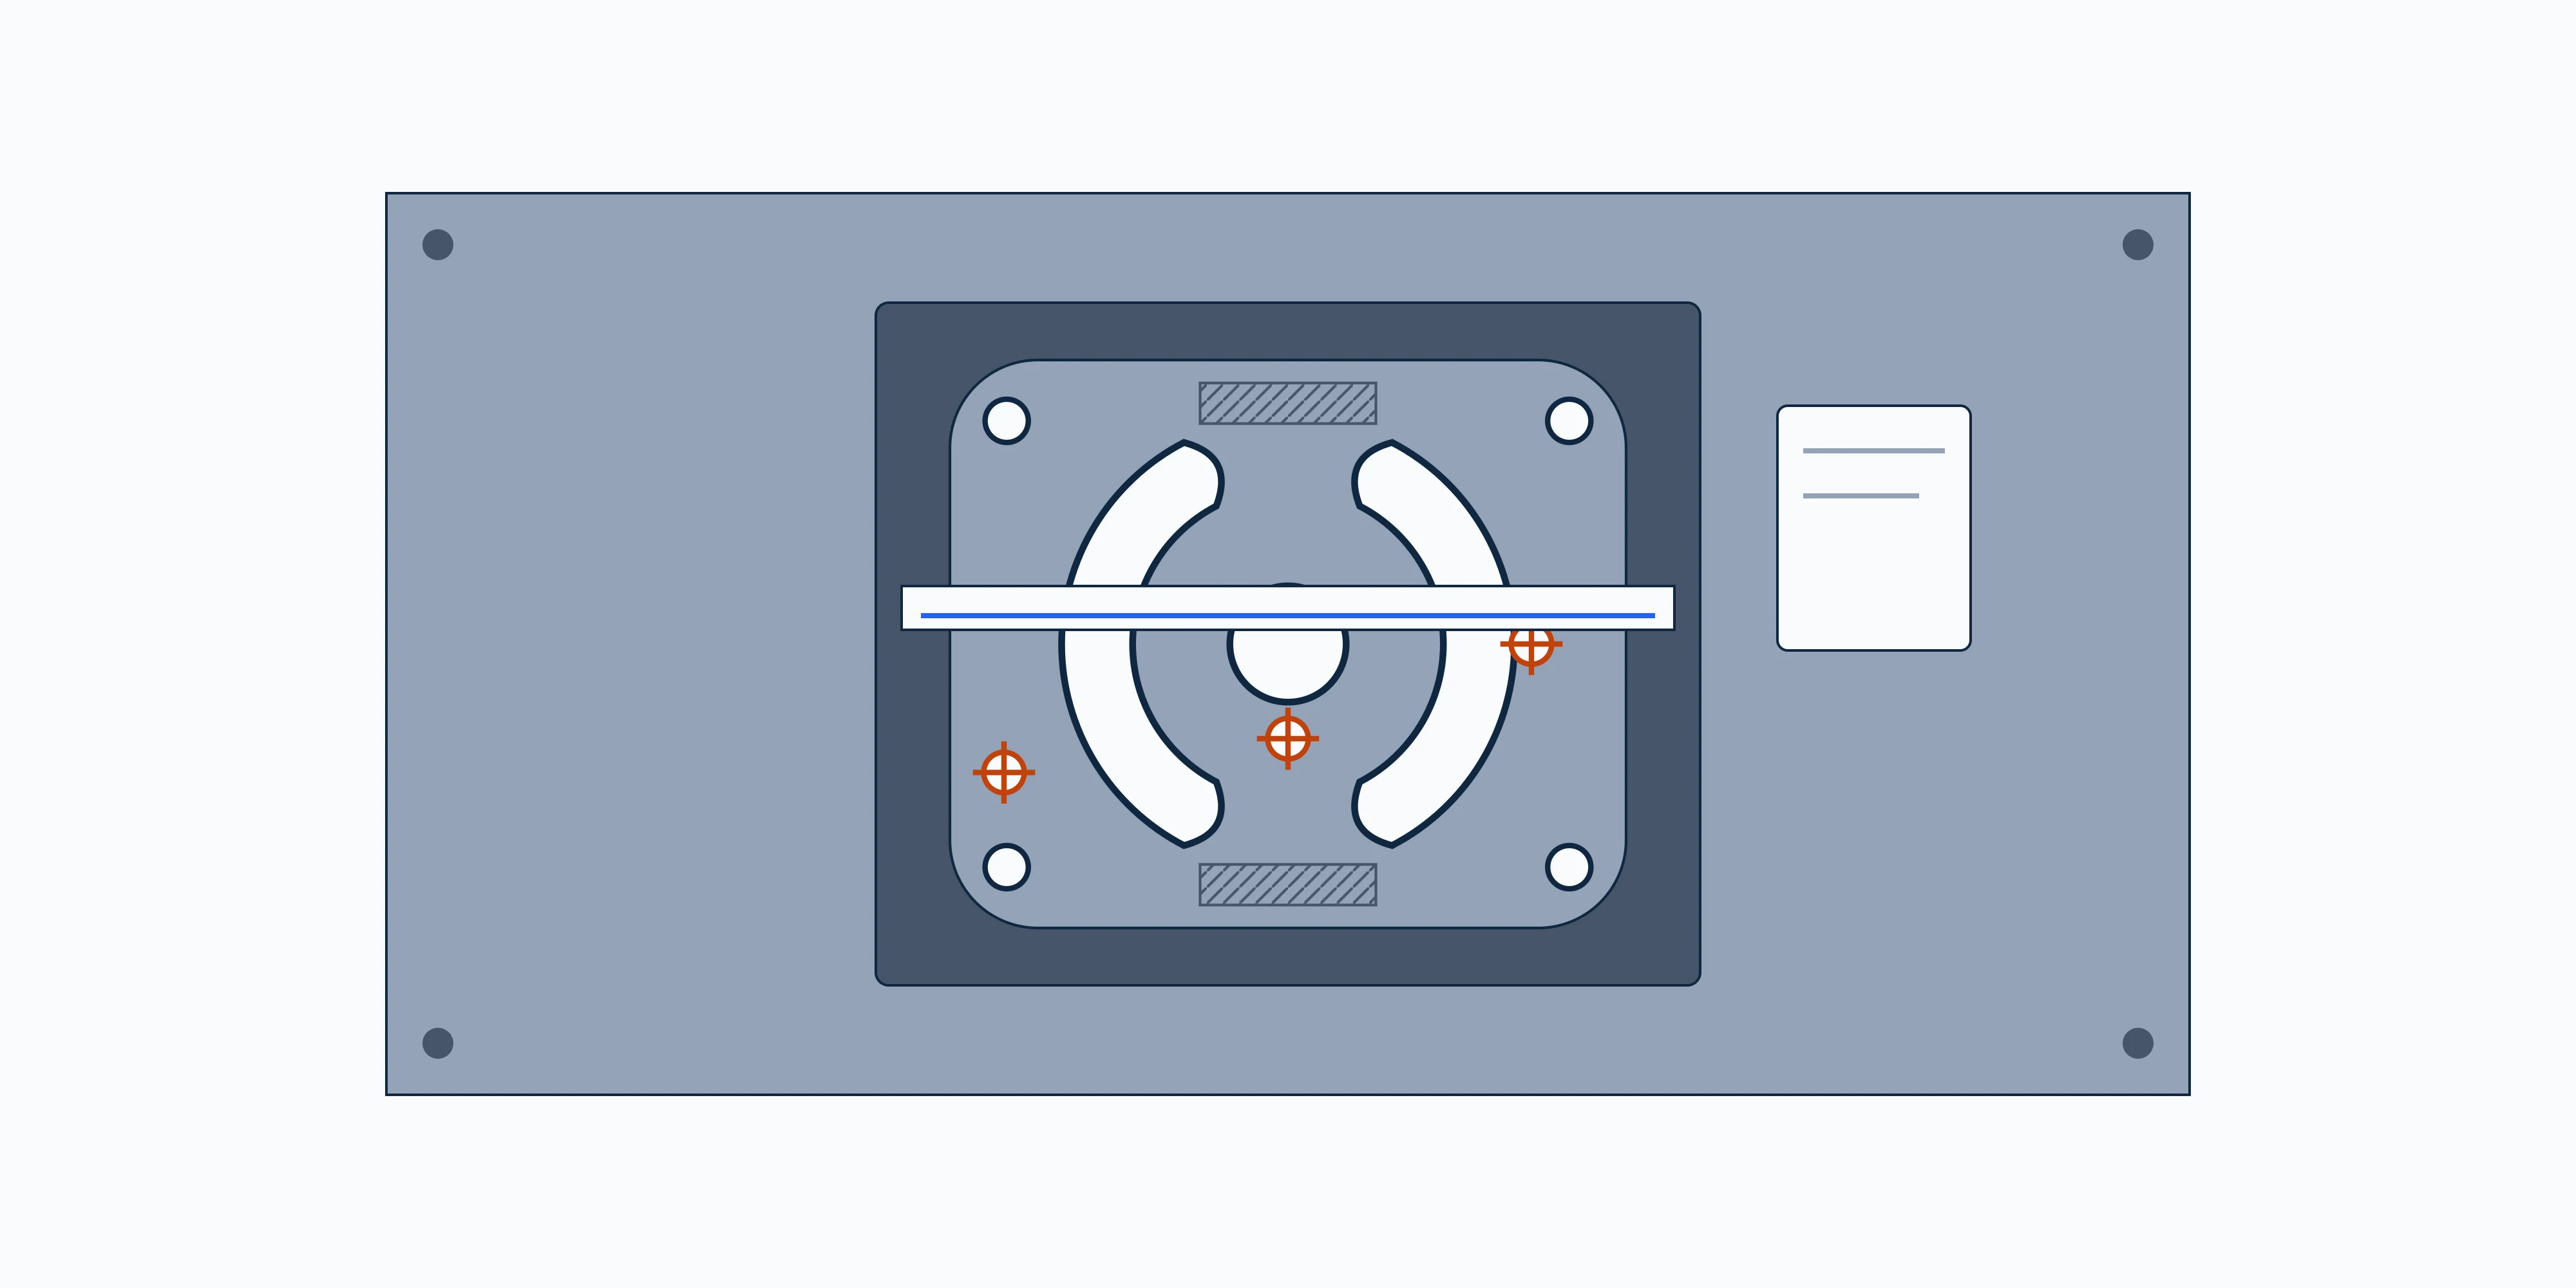
Valve plate inspection points: ground sealing face, ports, holding points and inspection locations
Where a valve plate is measured, and why the holding method affects the flatness result.

Flatness vs Surface Roughness: Two Different Quality Requirements

These two terms are often used as if they described the same thing. They do not, and treating them as one is the most common reason a valve plate grinding problem is misdiagnosed.

Flatness is form

Flatness describes how far the face deviates from a plane. It is a geometric property of the whole surface, measured against a reference — for example on a surface plate, with a straightedge and gauge, or by a coordinate measuring method. It says nothing about how rough the surface is.

Surface roughness is texture

Roughness describes the small-scale peaks and valleys left by the abrasive. It is measured across the surface with a profilometer and reported as a parameter such as Ra or Rz, with the cut-off and direction stated. It says nothing about whether the face is flat.

The four combinations are all real

A face can be flat and smooth, flat and rough, smooth but not flat, or rough and not flat. Each combination points at a different cause. Writing only one of the two requirements on an inquiry makes it impossible to tell which case is being dealt with.

A finer grit does not correct flatness

Grit size changes the texture. If the face is out of flat because of clamping, magnetic holding, heat, stock variation or a worn wheel, a finer wheel will usually make the texture number look better while the form problem remains — or gets worse, because a finer wheel cuts cooler but loads more readily.

State the measurement method

Two parties can measure the same face and disagree because they used different references, different cut-offs or different inspection positions. Record the instrument, the reference and the location on the face for both flatness and roughness.

Flatness and surface roughness compared: four combinations of form and texture
Flatness is form; roughness is texture. A face can pass one and fail the other.

Conventional Grinding Wheels vs CBN: When to Consider Each

These are the two families most often compared for valve plate face grinding. The decision is not about which is better; it is about which fits the material, the machine and the production pattern.

Conventional abrasives: the usual starting point

Aluminium oxide and silicon carbide wheels in a suitable bond cover a wide range of cast iron and steel plates, and they tolerate a variety of machines and fixtures. They are commonly the first family to evaluate on mixed or lower-volume work, where the process is still being established. Dressing is straightforward and the cost of changing specification is low.

CBN: evaluate for hard ferrous plates in stable production

CBN is a superabrasive intended for hard ferrous materials. It becomes worth evaluating when the plate material is hard, the specification is stable, the machine is rigid and the coolant delivery is under control. It is not a default upgrade: a machine that cannot support it, or a process that is still changing, will not benefit from it.

Diamond: a qualified discussion, not a general choice

Diamond is not a general-purpose abrasive for ferrous valve plates. At grinding temperature diamond reacts with iron, which leads to rapid abrasive wear. Diamond belongs to non-ferrous and very hard non-metallic work — for example certain carbide or ceramic features, or specific bronze applications — and even there it has to be justified by the material and the process, not assumed.

Match the bond and structure to the operation

Within either family, the bond system and the wheel structure decide how freely the wheel cuts, how it holds form and how often it needs dressing. Those choices follow from the plate material, the contact area and the coolant, not from the abrasive name alone.

Do not decide from the part name

'Valve plate' does not identify an abrasive. Two plates with the same drawing number but different material, hardness or hardened depth may need different families. Decide from the material record and the failure mode.

Where the operation appears

Valve plate grinding situations this guide covers

The same wheel question produces different answers depending on which plate is on the table. Review each materially different plate as its own record.

Hydraulic pump valve plate faces

The main sealing face that runs against the rotating group. Face-ground for form and texture; typically the operation this article is written for.

Hydraulic motor valve plates

Similar face grinding requirement to pump plates, but the duty cycle and the distortion pattern can differ. Review separately rather than copying a pump plate specification.

Multi-material and bimetal plates

Plates that combine a steel body with a bronze or other bearing overlay, or that present more than one material at the ground face.

Material matters

The plate material decides the abrasive family

Do not assume all hydraulic valve plates are the same material. Steel, cast iron, bronze and multi-material plates behave differently at the wheel face, and the correct abrasive family follows from that — not from the part name.

Hardened and alloy steels

Ferrous plates where the face may be through-hardened or case-hardened. Hardness, the depth of the hardened layer and the risk of tempering at the surface all affect wheel choice. CBN becomes worth evaluating where the material is hard and the production is stable.

Cast iron plates

Graphite in the structure changes how the wheel cuts and how it loads. Conventional abrasives are usually the first family reviewed. Porosity and occasional hard spots affect consistency, so the casting source and any variation should be stated.

Bronze and copper-alloy plates

Soft, non-ferrous and prone to smearing rather than cutting cleanly. Wheel openness, bond and coolant delivery matter more than hardness alone. This is a separate review from a steel plate, not a variation of it.

Multi-material / bimetal plates

A steel body with a non-ferrous overlay, or a face that presents more than one material. The wheel leaves one material and enters another within the same pass, so no single grade can be assumed. State the layer order and thickness.

Coated or surface-treated faces

Where the ground face is a coating rather than base metal, the wheel is cutting a different material than the drawing suggests. Identify the coating type and thickness before selection.

Diagnostic Guide

Common Valve Plate Grinding Problems

The quality of the wheel recommendation depends on the quality of the application record. These three practices prevent most of the back-and-forth.

The same defect name can come from the wheel, the coolant, the dressing condition, the fixture or the machine. Use this table to decide what to check before changing a specification.

Problem

Grinding burn

What you see

Discolouration, tempering tint or a patch that looks different from the surrounding face; sometimes a faint pattern following the wheel path.

Likely contributors

Heat at the contact zone from a wheel that is too hard or too fine for the material, a wheel that has stopped cutting freely, insufficient coolant reaching the contact, or a heavy stock removal pass.

What to check first

Confirm the wheel grade and structure against the material, the dressing condition, coolant type, flow and nozzle aim, and the stock allowance per pass. Record where on the face the burn appears.

Problem

Wheel loading

What you see

Metal or workpiece material packed into the wheel face; the wheel looks glazed or shiny, and the face finish deteriorates while the wheel stops cutting.

Likely contributors

A wheel that is too hard or too dense for a soft or gummy material, poor coolant delivery to the contact zone, or insufficient dressing to keep the face open. Common on bronze and other non-ferrous plates.

What to check first

Inspect the wheel face, not only the workpiece. Review coolant delivery, dressing frequency and tool condition, and whether the bond and structure suit the plate material.

Problem

Poor surface finish

What you see

Roughness above the drawing requirement, visible scratch pattern, chatter marks or a finish that varies across the face.

Likely contributors

Grit or bond not matched to the roughness requirement, a wheel that is not dressed cleanly, machine or fixture vibration, an unbalanced wheel, or a dressing tool that is dull or incorrectly applied.

What to check first

Confirm the roughness parameter and cut-off, the dressing tool and its condition, wheel balance, fixture rigidity, and whether the finish varies with position on the face.

Problem

Flatness deviation

What you see

The face does not seat or measures out of flat — often centre high or low, dished, or distorted near clamping points and ports.

Likely contributors

Clamping or magnetic holding distortion of a thin plate, heat built up during grinding, residual stress from earlier operations or hardening, an uneven stock allowance, or a wheel that is not cutting evenly across the face.

What to check first

Measure the face as held and as released, mark the inspection positions, and compare the flatness result with the roughness result. Review fixture design, magnetic holding, coolant and stock distribution.

Problem

Excessive dressing

What you see

The wheel needs dressing far more often than expected, wheel consumption is high, or the face finish drifts between dresses.

Likely contributors

A wheel grade or bond that is too hard for the operation and is being forced to cut, a dressing tool that is dull or applied at the wrong conditions, or a process compensating for another problem by dressing repeatedly.

What to check first

Record dressing frequency, tool type and condition, and the reason each dress is made. Compare with the wheel specification and the material.

Fast diagnostic flow

Quick decision flow

  1. 1

    Plate is cast iron or general steel, volume is mixed or still being established

    Evaluate a conventional aluminium oxide or silicon carbide wheel in a suitable bond first.

  2. 2

    Plate is hard ferrous material, specification is stable, machine is rigid

    Evaluate CBN against the same acceptance requirements as the current wheel.

  3. 3

    Plate is bronze or another soft non-ferrous material

    Treat as a new application: review wheel openness, bond and coolant before grade.

  4. 4

    Face is smooth but not flat

    Check clamping, magnetic holding, heat and stock distribution — not the grit size.

  5. 5

    Face is flat but too rough

    Check dressing, balance and vibration first, then grit and bond against the requirement.

  6. 6

    Burn or loading keeps returning after dressing

    Review coolant delivery and the wheel specification together with the supplier.

Send the defect photograph, the face drawing and the current wheel specification for an application review.

Send a valve plate application →
Wheel selection matrix by valve plate material, abrasive family and decision factors
Material comes first. Match the abrasive family to the plate, then refine grit, grade, bond and structure.

Workpiece material, abrasive family and decision factors

A starting map for the review — not a recommendation. Each row still requires the plate drawing and the acceptance requirements.

Hardened / alloy steel plate

Abrasive family to evaluate first
Conventional aluminium oxide; CBN where hard, stable and supported by the machine
Grinding concern to watch
Burn and tempering at the face; wheel form retention
Decision factors
Hardness and hardened depth, machine rigidity, coolant delivery, production stability

Cast iron plate

Abrasive family to evaluate first
Conventional silicon carbide or aluminium oxide
Grinding concern to watch
Loading, hard spots, consistency between castings
Decision factors
Casting source and variation, porosity, coolant cleanliness, dressing practice

Bronze / copper-alloy plate

Abrasive family to evaluate first
Open-structure conventional wheel with suitable bond
Grinding concern to watch
Smearing and loading rather than burn
Decision factors
Alloy, coolant type and delivery, wheel openness, dressing frequency

Multi-material / bimetal plate

Abrasive family to evaluate first
Split review per layer; no single grade assumed
Grinding concern to watch
Different behaviour as the wheel crosses materials
Decision factors
Layer order and thickness, where the wheel transitions, fixture support

Coated / surface-treated face

Abrasive family to evaluate first
Determined by the coating, not the base metal
Grinding concern to watch
Coating removal versus base metal cutting
Decision factors
Coating type and thickness, allowance, whether the coating must be preserved
Plate materialAbrasive family to evaluate firstGrinding concern to watchDecision factors
Hardened / alloy steel plateConventional aluminium oxide; CBN where hard, stable and supported by the machineBurn and tempering at the face; wheel form retentionHardness and hardened depth, machine rigidity, coolant delivery, production stability
Cast iron plateConventional silicon carbide or aluminium oxideLoading, hard spots, consistency between castingsCasting source and variation, porosity, coolant cleanliness, dressing practice
Bronze / copper-alloy plateOpen-structure conventional wheel with suitable bondSmearing and loading rather than burnAlloy, coolant type and delivery, wheel openness, dressing frequency
Multi-material / bimetal plateSplit review per layer; no single grade assumedDifferent behaviour as the wheel crosses materialsLayer order and thickness, where the wheel transitions, fixture support
Coated / surface-treated faceDetermined by the coating, not the base metalCoating removal versus base metal cuttingCoating type and thickness, allowance, whether the coating must be preserved

Separate the two quality requirements

Flatness is form; roughness is texture. They are produced by different parts of the process and measured with different equipment. Putting them in one line on an inquiry hides which one is failing.

  • Flatness: measured against a plane, with the method stated
  • Roughness: measured across the surface, with the parameter stated
  • A surface can pass one and fail the other

Diagnose before changing the wheel

Burn, loading and flatness drift can each come from the wheel, the coolant, the dressing condition, the fixture or the machine. Changing the grade first removes the evidence.

  • Record the defect location, not just its name
  • Check dressing and coolant before changing specification
  • Photograph the face and the wheel surface

Keep the review material-specific

A specification carried over from a steel plate to a bronze plate, or from a large plate to a thin one, is an untested assumption. Review each material and each fixture separately.

  • One record per materially different plate
  • State the hardened layer or coating, not only the base metal
  • State the stock allowance and where it sits

Decision checklist

A practical valve plate grinding wheel selection checklist

Work down this list before choosing a specification. Each line changes the answer, and several of them cost nothing to collect.

1. Identify the plate material and its condition: base metal, hardened layer or coating. State the hardness only if it is actually known from the drawing or a measurement.

2. Write flatness and surface roughness as two separate line items, each with its requirement, its measuring method and the current result.

3. Describe the ground face: width, whether ports or recesses interrupt the contact, and where the wheel enters and exits.

4. State the stock allowance and whether the plate is ground from solid or after a previous operation.

5. Describe the workholding: how the plate is clamped or held magnetically, and whether the fixture itself influences flatness.

6. Record the machine: type, spindle capability and the coolant type and delivery method.

7. Record dressing practice: tool type, frequency, and whether the wheel is dressed in or out of the machine.

8. Name the current failure mode and where it appears on the face — centre, edge, near ports, or across the whole face.

9. Compare wheel families only after the material and the failure mode are established. Do not start from a grade number.

10. If the plate is non-ferrous or multi-material, treat the review as a new application rather than adapting a steel plate record.

What to send

What Information Is Needed for a Custom Grinding Wheel Quote?

A wheel recommendation can only be as specific as the application record behind it. These items let the review start from the actual face requirement instead of from a wheel name.

  • Plate drawing with the ground face, its width, and any ports, recesses or interrupted contact

  • Plate material, condition (base metal, hardened layer or coating) and the known hardness if it is on the drawing

  • Flatness requirement, measuring method and current measured result

  • Surface roughness requirement (parameter, value and cut-off), measuring method and current result

  • Stock allowance, and whether the plate is ground from solid or after a previous operation

  • Workholding method and fixture details, including magnetic holding if used

  • Machine type, spindle capability, coolant type and delivery method

  • Current wheel specification, dimensions and marking

  • Dressing tool, dressing frequency and dressing method

  • Photographs of the plate face, the wheel face and the defect, with the defect location marked

Send these details through the inquiry form, or contact us on WhatsApp for a preliminary recommendation.

Send Grinding Details →

Where it is used

Industries grinding valve plates

Valve plates appear wherever positive-displacement hydraulic components are made or rebuilt. The grinding review is the same in principle; the acceptance requirements come from the component's duty.

Hydraulic pump manufacturing
Hydraulic motor manufacturing
Fluid power component remanufacturing
Precision machining subcontracting

FAQ

Frequently Asked Questions

Direct answers to the questions that most often come up before a valve plate wheel is selected.

What grinding wheel is used for hydraulic valve plates?

It depends on the plate material and the face requirement. For many cast iron and general steel plates, a conventional aluminium oxide or silicon carbide wheel in a suitable bond is the first family to evaluate. Hardened ferrous plates in stable production may justify evaluating CBN. Bronze and multi-material plates need their own review. There is no single specification that covers all valve plates.

Why does a smooth valve plate still leak?

Because surface roughness and flatness are different properties. A face can measure smooth and still be out of flat, typically because of clamping or magnetic holding distortion, heat during grinding, residual stress or uneven stock removal. Roughness cannot compensate for a form error.

Can a finer grit fix flatness problems on a valve plate?

No. Grit size changes surface texture, not form. If the plate is not flat, the cause is usually in workholding, heat, residual stress or stock distribution. A finer wheel can even make things worse by loading more readily and cutting less freely.

Should I use a CBN wheel for valve plate grinding?

Evaluate CBN when the plate is a hard ferrous material, the specification is stable, the machine is rigid enough and coolant delivery is under control. It is not an automatic upgrade. For mixed or lower-volume work on softer materials, a conventional wheel is usually the sensible starting point.

Can diamond wheels be used on hydraulic valve plates?

Not as a general choice for ferrous plates. Diamond reacts with iron at grinding temperature, causing rapid abrasive wear. Diamond belongs to non-ferrous and very hard non-metallic work, and even there it must be justified by the specific material and process rather than assumed suitable.

How do I describe grinding burn versus loading?

Burn appears as discolouration, tempering tint or a heat-affected patch on the workpiece face. Loading is material packed into the wheel face, which makes the wheel look glazed or shiny and stops it cutting. Send a photograph of both the plate face and the wheel face — they point to different causes.