Grinding Wheel Recommendation: What Information Helps Match the Right Wheel

Grinding Wheel Knowledge Base

Grinding Wheel Recommendation: What Information Helps Match the Right Wheel

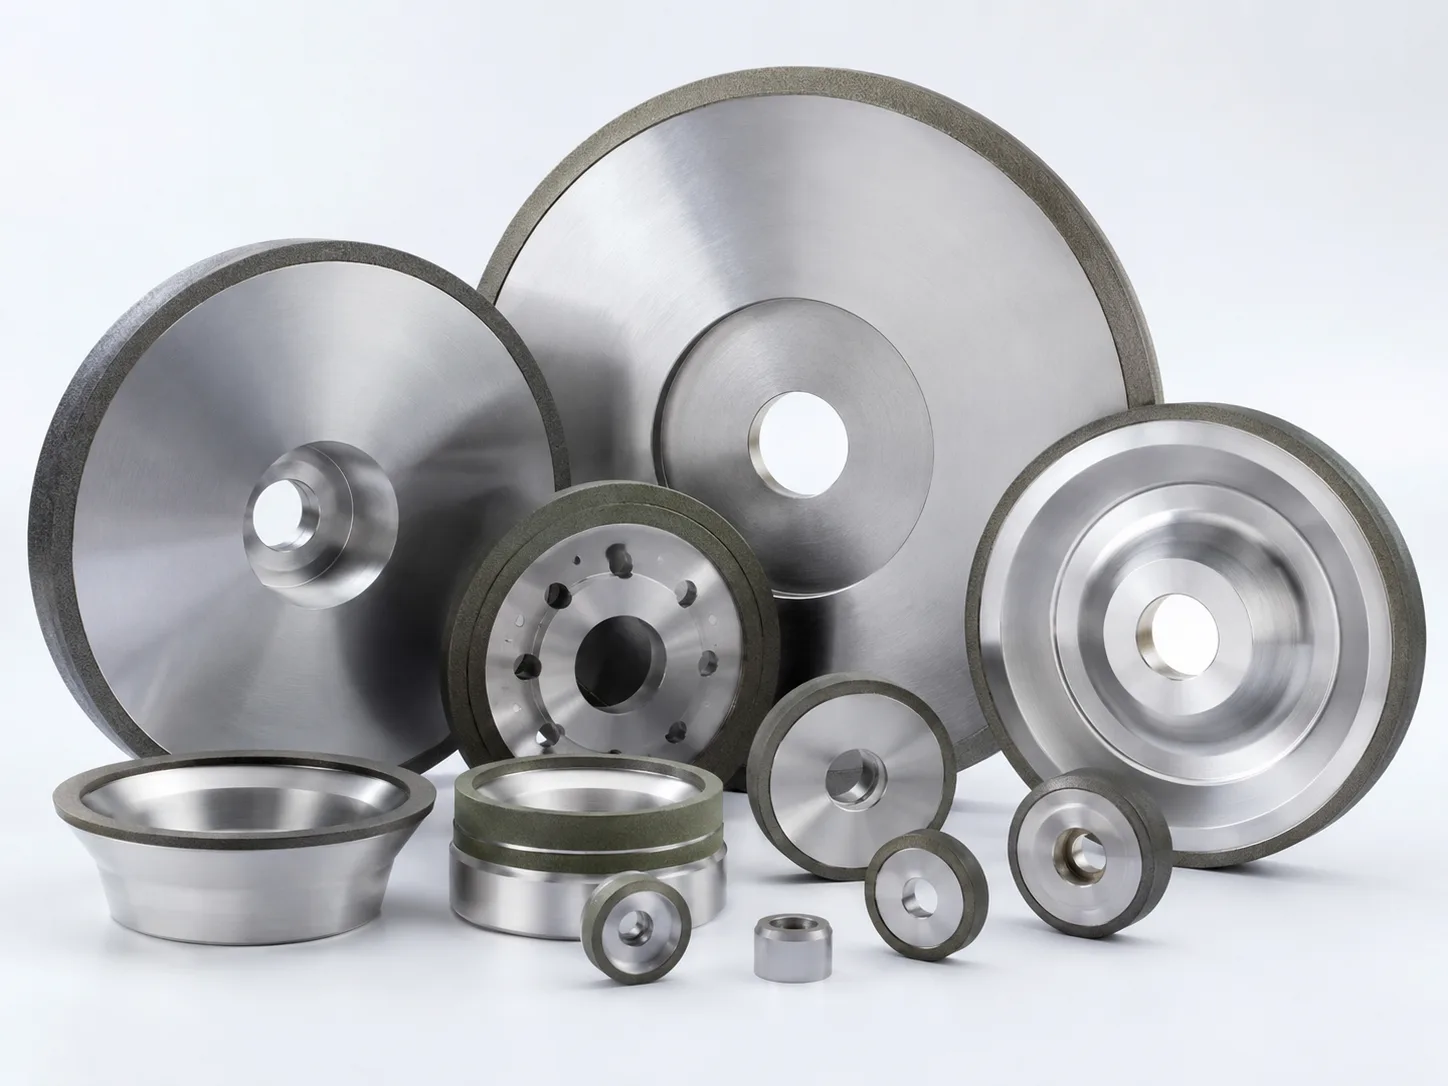
A useful grinding wheel recommendation begins with the real grinding application, not only a wheel name, size, photo, or material label. Workpiece material and hardness, machine type and rigidity, grinding position, coolant, dressing, contact area, current wheel specification, observed problem, and required result all give the supplier a different part of the review context.

Send the application conditions, not only the grinding wheel name or size
Material, machine, coolant, dressing and the current problem must be reviewed together
A photo can support identification, but dimensions, drawing and application details are more reliable
Final suitability may still require sample confirmation or a controlled trial

Overview

Quick answer: send the application, not only the wheel

Before asking for a grinding wheel recommendation, prepare the workpiece material and hardness, grinding operation, machine type, wheel size and existing marking, wet or dry condition, coolant and dressing details, the current problem, and the result you are trying to hold. Add a dimensioned drawing, clear photos, or a sample reference when available. This information helps the supplier decide whether the inquiry is complete enough for an initial review and which comparison should come next.

A recommendation is an application-based review of possible wheel directions. It is not a promise that one specification will suit every machine or every production condition. The review may compare abrasive type, bond, grit size, wheel grade, structure, shape, profile, or a custom construction, but those fields only become meaningful when connected to the workpiece, machine, coolant, dressing method, contact area, process symptoms, and acceptance target.

What a useful recommendation needs

  • Material and hardness help screen abrasive and bond directions, but they do not complete the wheel selection.
  • Machine condition, contact area, coolant delivery and dressing can change how the same wheel behaves.
  • Loading, glazing, burn marks, fast wear, chatter and unstable finish point to different review paths.
  • Unknown information should be marked as unknown rather than replaced with an estimate.
Industrial application review map showing material, machine, coolant, current problem, grinding wheel and technical drawing information
A recommendation should connect the workpiece, machine, coolant, observed problem, wheel details and supporting evidence as one application set.

What does a grinding wheel recommendation mean?

A supplier-side application review translates confirmed grinding conditions into possible specification directions and identifies what still needs confirmation.

It starts with the real grinding operation

Surface, external cylindrical, internal, centerless, profile and other grinding positions create different contact, access, stock-removal and wheel-shape requirements. The operation must be stated before a wheel direction can be reviewed.

It compares interacting specification fields

Abrasive, bond, grit size, wheel grade, structure, concentration where applicable, shape and profile interact. Reviewing one field in isolation can hide the reason the present wheel behaves as it does.

It separates confirmed facts from open questions

A preliminary review may identify a conventional, CBN, diamond or custom wheel direction while leaving dimensions, mounting, dressing, coolant, trial conditions or acceptance criteria for confirmation.

Workpiece material and hardness

Material identity and hardness are the first technical filters because they affect abrasive compatibility, chip behavior, heat, grain wear and bond demand.

State the material grade when known

A broad label such as steel, carbide, ceramic or glass may be a useful starting point, but grade, composition, coating, heat treatment and surface condition can change the review. If the grade is unknown, state that clearly.

Share hardness and heat-treatment condition

The same material family can create a different grinding demand at another hardness or after a heat-treatment change. Provide the measurement scale and value only when confirmed.

Describe mixed or coated contact

If the wheel crosses a coating, binder, braze, interrupted feature or more than one material, describe what reaches the grinding zone. The review should not assume the contact is uniform.

Machine type, rigidity and grinding position

A wheel that is reasonable on one machine may not behave the same way when spindle condition, rigidity, speed range, power, mounting, guarding or contact geometry changes.

Identify the machine and mounting arrangement

Share the machine manufacturer and model when available, spindle or arbor arrangement, available speed range, mounting method and any relevant guarding limit. A photo of the mounting area can support, but not replace, dimensions.

Describe the grinding position and contact area

State where the wheel contacts the workpiece, the approximate contact width or arc, whether contact is continuous or interrupted, and whether the wheel works on a face, diameter, edge, groove or profile.

Report vibration or rigidity concerns

Chatter, spindle play, weak fixturing, balance condition or an unstable setup can affect finish and wheel behavior. These observations belong in the application review rather than being treated automatically as a wheel-specification issue.

Coolant condition and dressing condition

Coolant and dressing directly affect the active wheel surface, heat removal, chip clearance, profile and the point at which grinding performance begins to change.

State wet or dry grinding

For wet grinding, include coolant type when known, concentration when measured, filtration condition, nozzle direction and whether flow reaches the contact zone. Note recent coolant or delivery changes.

Describe how the wheel is prepared

Share the dressing or truing tool, method, frequency, trigger and tool condition. If the wheel is not dressed in the current process, say so. Different wheel systems may require different preparation capability.

Photograph surface evidence before dressing

When loading, glazing or localized wear matters, a clear wheel-surface photo before dressing can preserve evidence. Add coolant and dressing information so the photo is not interpreted without process context.

Wheel size, shape and existing specification

Physical fit and the current wheel reference help define the review, but neither explains the complete grinding demand by itself.

Provide confirmed wheel dimensions

State outside diameter, bore, thickness and profile dimensions. For superabrasive wheels, include abrasive-layer location and dimensions when known. A dimensioned drawing is more reliable than a perspective photo for geometry.

Copy the complete existing marking

Include abrasive, bond, grit, wheel grade, structure or concentration, shape, size and manufacturer code as shown. Do not infer a missing specification from color or appearance.

Explain what should remain and what may change

If mounting, geometry or an approved process condition must remain fixed, say so. Also identify whether the inquiry is about replacing a known wheel, correcting a symptom, comparing wheel types or reviewing a custom shape.

Common mistakes when asking for a recommendation

An incomplete message can still start a conversation, but it should not be treated as enough for a final wheel decision.

Sending only the wheel size

Size confirms possible fit, not abrasive compatibility, contact demand, dressing needs, coolant access or the result the process must hold.

Sending one photo without dimensions

A photo can help identify general shape and condition, but perspective can hide bore, thickness, profile and mounting details. Add measurements or a drawing.

Naming only the workpiece material

Material without hardness, grinding operation, contact, machine, coolant, stock and finish target leaves too many possible wheel directions open.

Describing a symptom without timing

State whether loading, glazing, burn, chatter, rapid wear or finish drift appears immediately, after dressing, after a material change or after a certain part of the cycle.

Guessing missing technical details

An unknown value is useful when marked unknown. An estimated speed, hardness, dimension or wheel code presented as exact can send the review in the wrong direction.

Changing several factors at once

If abrasive, grit, bond, wheel grade, coolant, dressing and parameters all change together, the next result may be difficult to interpret. Keep the comparison controlled where practical.

When a controlled trial may still be needed

A complete application review can narrow the specification direction, but it cannot reproduce every machine, dressing, coolant and production condition remotely.

New or uncertain applications

When there is no stable current wheel, limited material information or an unfamiliar contact condition, sample confirmation and a controlled trial may be needed before a production decision.

Custom shape, profile or mounting

Confirm drawings, mounting, clearances and usable abrasive area before the trial. Geometry approval and grinding suitability are related but separate review steps.

Abrasive-system changes

A change between conventional, CBN and diamond wheel systems may require a review of machine speed, rigidity, coolant, dressing or truing capability and process controls before comparison.

How to make the comparison useful

Hold the material, machine, dressing, coolant, stock and measured acceptance criteria as consistently as practical. Record what changed and compare the same observations without assuming the outcome.

Application Context

Why one grinding wheel cannot fit every application

The wheel name and dimensions may look similar while the real grinding demand changes. These examples show why the application context must travel with the inquiry.

Same material, different hardness

Confirm material grade, hardness scale, heat treatment, coating and stock condition.

Review abrasive compatibility and wheel behavior against the actual hardness and grinding contact.

Same wheel, different machine

Share machine model, spindle condition, mounting, available speed and vibration observations.

Check machine readiness before treating the current wheel specification as directly transferable.

Same specification, different coolant

Describe coolant type, condition, nozzle direction, flow access and recent changes.

Review coolant and wheel-surface condition together before changing wheel fields.

Same symptom, different cause

Record when the symptom appears and what changed in material, dressing, coolant, machine or parameters.

Use the symptom to choose checks, not to assume one universal replacement wheel.

Conditional Comparison

Conventional, CBN, diamond or custom: what may need review

Abrasive type is a review direction, not a complete recommendation. Compare the whole wheel system and the actual grinding conditions before deciding.

Conventional grinding wheels

Often reviewed across general ferrous and non-ferrous grinding with abrasive, bond, grit, wheel grade and structure selected conditionally for the material, contact, machine, dressing and coolant.

CBN grinding wheels

Commonly considered for suitable hardened ferrous workpiece materials, subject to machine readiness, wheel speed, contact, bond, coolant and dressing or truing capability.

Diamond grinding wheels

Commonly considered for carbide, ceramic, glass and other hard non-ferrous or non-metallic workpiece contexts, with bond, concentration, coolant, contact and machine conditions still requiring review.

Custom grinding wheels

May be reviewed when standard geometry, abrasive-layer design, mounting or specification options do not match the confirmed application. Feasibility and suitability still need technical confirmation.

Diagnostic Guide

Buyer situations and useful application-review directions

The same request for a grinding wheel recommendation can begin with a different symptom, comparison or unknown. Each situation needs a focused information set.

Start with the observed situation, then collect the evidence that can distinguish wheel specification from machine, coolant, dressing or process conditions.

Buyer situation

Wheel wears too fast

Useful review direction

Compare grinding wear with material removed during dressing, then review wheel grade, bond, abrasive, grit, structure and operating demand.

What extra information helps

Current specification, diameter loss, dressing frequency and depth, stock, contact area, speed, coolant and photos before and after dressing.

Review boundary

Do not treat all diameter loss as wear created during grinding.

Buyer situation

Workpiece burn marks

Useful review direction

Review heat generation and heat removal across wheel sharpness, dressing, coolant delivery, stock, contact and operating parameters.

What extra information helps

Material and hardness, burn location, when it appears, coolant access, dressing condition, current wheel marking and process changes.

Review boundary

A wheel change is only one possible review path.

Buyer situation

Wheel loading

Useful review direction

Check whether workpiece material or chips are packing into wheel pores and whether the surface can clear material between contacts.

What extra information helps

Wheel-surface photo before dressing, material, coolant and filtration, dressing method, structure, bond, grit and contact area.

Review boundary

Separate loading from a shiny glazed surface.

Buyer situation

Wheel glazing

Useful review direction

Review whether abrasive points have become dull while the bond continues to retain them, together with dressing and grinding force.

What extra information helps

Surface photo, sound or force change, current wheel grade, bond, grit, dressing method, contact, speed and machine condition.

Review boundary

Confirm glazing before assuming the pores are filled with material.

Buyer situation

Chatter marks

Useful review direction

Compare wheel balance and condition with spindle, mounting, rigidity, fixturing, dressing and contact before changing the specification.

What extra information helps

Chatter pattern, machine model, wheel mounting, balance history, dressing setup, contact position, speed and photos of the result.

Review boundary

Machine or setup vibration may remain after a wheel change.

Buyer situation

Unstable surface finish

Useful review direction

Track whether finish changes with time after dressing, wheel loading or glazing, material variation, coolant condition or machine drift.

What extra information helps

Measured finish, sampling point, time after dressing, current specification, material batch, coolant, stock and dressing frequency.

Review boundary

State the measured target and the pattern of variation when available.

Buyer situation

Changing from a conventional wheel to CBN

Useful review direction

Review hardened ferrous material compatibility and whether the machine, speed, coolant, dressing or truing and process stability support comparison.

What extra information helps

Material and hardness, current cycle, wheel size, speed, machine rigidity, dresser, coolant, profile demand and reason for considering a change.

Review boundary

CBN is not an automatic replacement for a stable conventional process.

Buyer situation

Reviewing diamond vs CBN

Useful review direction

Start with exact workpiece material and ferrous or non-ferrous context, then compare complete wheel systems rather than abrasive names alone.

What extra information helps

Material grade, hardness, coating or binder, contact, bond, grit, concentration, coolant, machine and finish target.

Review boundary

Mixed or coated contact may require additional review.

Buyer situation

Custom wheel shape or unknown specification

Useful review direction

Separate geometry identification from grinding-performance review and confirm which dimensions or specification fields are unknown.

What extra information helps

Dimensioned drawing, clear wheel and label photos, mounting area, current application, material, machine, coolant, dressing and observed result.

Review boundary

One photo is not enough for final geometry or specification confirmation.

Industrial grinding wheel application checklist with material and hardness, machine and position, coolant and dressing, and current problem
These four information groups provide the minimum context for deciding what the next application-review questions should be.

Application details to send before asking for a recommendation

Use confirmed values where available and mark missing items as unknown. The examples are information formats, not target values.

Workpiece material

What to send
Material family and exact grade when known, plus coating, binder, scale or mixed-material contact.
Why it matters
Helps screen abrasive compatibility and chip behavior.
Example
Hardened ferrous steel, carbide grade, ceramic or glass workpiece context.

Workpiece hardness

What to send
Confirmed hardness value, scale and heat-treatment condition, or state that hardness is unknown.
Why it matters
Can change abrasive, bond and wheel-behavior review.
Example
Measured hardness with the stated scale rather than a broad label such as hard steel.

Grinding operation

What to send
Surface, external cylindrical, internal, centerless, profile or another defined grinding position.
Why it matters
Defines contact geometry, access, stock path and possible wheel shape.
Example
External cylindrical plunge grinding on a shoulder.

Machine type

What to send
Machine manufacturer and model when available, spindle or arbor, speed range, rigidity or vibration observations.
Why it matters
Shows machine capability and whether a wheel system is transferable.
Example
Machine model plus a clear mounting-area photo.

Coolant condition

What to send
Wet or dry grinding; coolant type, measured concentration, filtration, nozzle position and access when known.
Why it matters
Affects heat removal, chip clearance and wheel-surface condition.
Example
Wet grinding with filtered coolant directed at the contact zone.

Dressing condition

What to send
Dressing or truing tool, method, frequency, trigger and tool condition.
Why it matters
Changes wheel sharpness, profile, openness and apparent wheel loss.
Example
Dressing is triggered when finish begins to drift; method and tool are identified.

Current wheel size

What to send
Outside diameter, bore, thickness, profile and abrasive-layer dimensions where applicable.
Why it matters
Confirms fit, geometry and usable abrasive area.
Example
A dimensioned drawing that clearly separates bore, thickness and profile.

Existing wheel marking

What to send
Complete label or marking for abrasive, bond, grit, grade, structure or concentration, size, shape and code.
Why it matters
Provides a controlled reference for comparison.
Example
A sharp label photo plus the marking copied into the message.

Current grinding problem

What to send
Observable symptom, location, when it starts, how it changes and what changed before it appeared.
Why it matters
Chooses the review path and prevents unrelated specification changes.
Example
Loading appears after dressing and increased after a coolant-delivery change.

Surface finish or tolerance target

What to send
Required and measured values with method when available; otherwise describe the acceptance issue without inventing a value.
Why it matters
Clarifies what the process must hold and how a trial will be judged.
Example
Measured finish trend before and after dressing using the same inspection method.

Quantity or trial plan

What to send
Expected trial quantity, production pattern and which observations will be recorded.
Why it matters
Supports a controlled comparison without predetermining the result.
Example
A small trial under documented material, coolant and dressing conditions.

Drawing, photo or sample

What to send
Dimensioned drawing, wheel and label photos, mounting photo, problem evidence and sample reference when available.
Why it matters
Reduces geometry ambiguity and preserves visual evidence.
Example
A drawing for dimensions and separate photos for condition and mounting.
Workflow for collecting material, wheel size, photo or drawing and current grinding problem before sending a grinding wheel recommendation inquiry
Collect the confirmed application facts, send them through WhatsApp or the recommendation form, and allow open questions to be identified during the review.

Before Requesting a Recommendation

Simple application review checklist

Use this sequence to prepare a clear grinding wheel inquiry without trying to select every specification field yourself.

1. Define the grinding operation and where the wheel contacts the workpiece.

2. Record workpiece material, exact grade, hardness and heat-treatment or coating condition when known.

3. Measure the current wheel and attach a dimensioned drawing or clear photos of the wheel, marking, mounting and working surface.

4. Copy the current wheel specification without guessing missing fields.

5. Add machine model, mounting, speed range, grinding position, contact area and any rigidity or vibration concern.

6. Describe wet or dry grinding, coolant delivery and filtration, plus dressing or truing method and frequency.

7. State the present problem or target, when it appears, what changed and what measurement or observation shows it.

8. Mark unknown information clearly and agree on what must be confirmed before sample review or a controlled trial.

WhatsApp or Recommendation Form

What to send for a grinding wheel application review

A complete first message does not need every technical field, but it should give enough context to identify missing information and a useful review path.

  • Workpiece material and hardness

    Include the exact grade, heat treatment, coating or mixed contact when known.

  • Grinding operation and contact

    State the grinding position, contact area, stock and where the wheel works on the part.

  • Machine and mounting

    Share the machine model, spindle or arbor, speed range and mounting photo when available.

  • Wheel size and shape

    Provide outside diameter, bore, thickness, profile and abrasive-layer dimensions where applicable.

  • Existing wheel marking

    Copy the complete specification and attach a sharp label photo.

  • Coolant and dressing

    Describe wet or dry condition, coolant delivery, filtration, dressing or truing tool and frequency.

  • Current grinding problem

    Explain loading, glazing, burn marks, fast wear, chatter, finish drift or another observed issue and when it appears.

  • Target and evidence

    Add measured finish or tolerance information when confirmed, plus drawings, photos, sample references and a controlled trial plan.

Send your material, wheel size, photos, drawing and current grinding problem. We will review whether the information is enough for a grinding wheel recommendation.

Send Grinding Details →

FAQ

Questions about grinding wheel recommendations

These answers explain what an initial supplier review can establish and what may still need confirmation.

Can I ask for a grinding wheel recommendation with only the wheel size?

You can start an inquiry with the size, but size only confirms part of the physical request. Material, hardness, operation, machine, coolant, dressing, contact and the current target or problem are needed for a meaningful application review.

Is one photo enough for a final recommendation?

No. A photo can help identify general shape, marking or surface condition, but dimensions, a drawing, current specification and application details are more reliable. Additional confirmation or a controlled trial may still be needed.

Which information matters most if I do not know the wheel specification?

Start with material and hardness, grinding operation, machine, wheel dimensions, wet or dry condition, dressing method, current problem and clear photos. Mark the specification as unknown instead of estimating it.

Does workpiece material determine the abrasive type by itself?

No. Material and hardness provide an important compatibility filter, but bond, grit, concentration or wheel grade, contact, machine, coolant, dressing, finish and stock also affect the review.

When should conventional, CBN and diamond grinding wheels be compared?

Compare them when the material context and process objective justify it, then review complete wheel systems. CBN is commonly considered for suitable hardened ferrous materials, while diamond is commonly considered for carbide, ceramics, glass and other hard non-ferrous or non-metallic contexts. Neither selection is automatic.

What if my grinding problem is loading, glazing or burn marks?

Name the symptom, show where and when it appears, photograph the wheel surface before dressing when relevant, and add material, coolant, dressing, machine, contact and current wheel information. These symptoms do not share one universal cause.

Can I send the information through WhatsApp?

Yes. Send confirmed application details, wheel and label photos, drawings and the current problem. The website recommendation form is also available when a structured information set is easier to prepare.

Why may a controlled trial still be necessary?

Remote review cannot reproduce every machine, mounting, dressing, coolant, contact and production condition. A controlled trial can compare a confirmed wheel direction under documented conditions before a production decision.