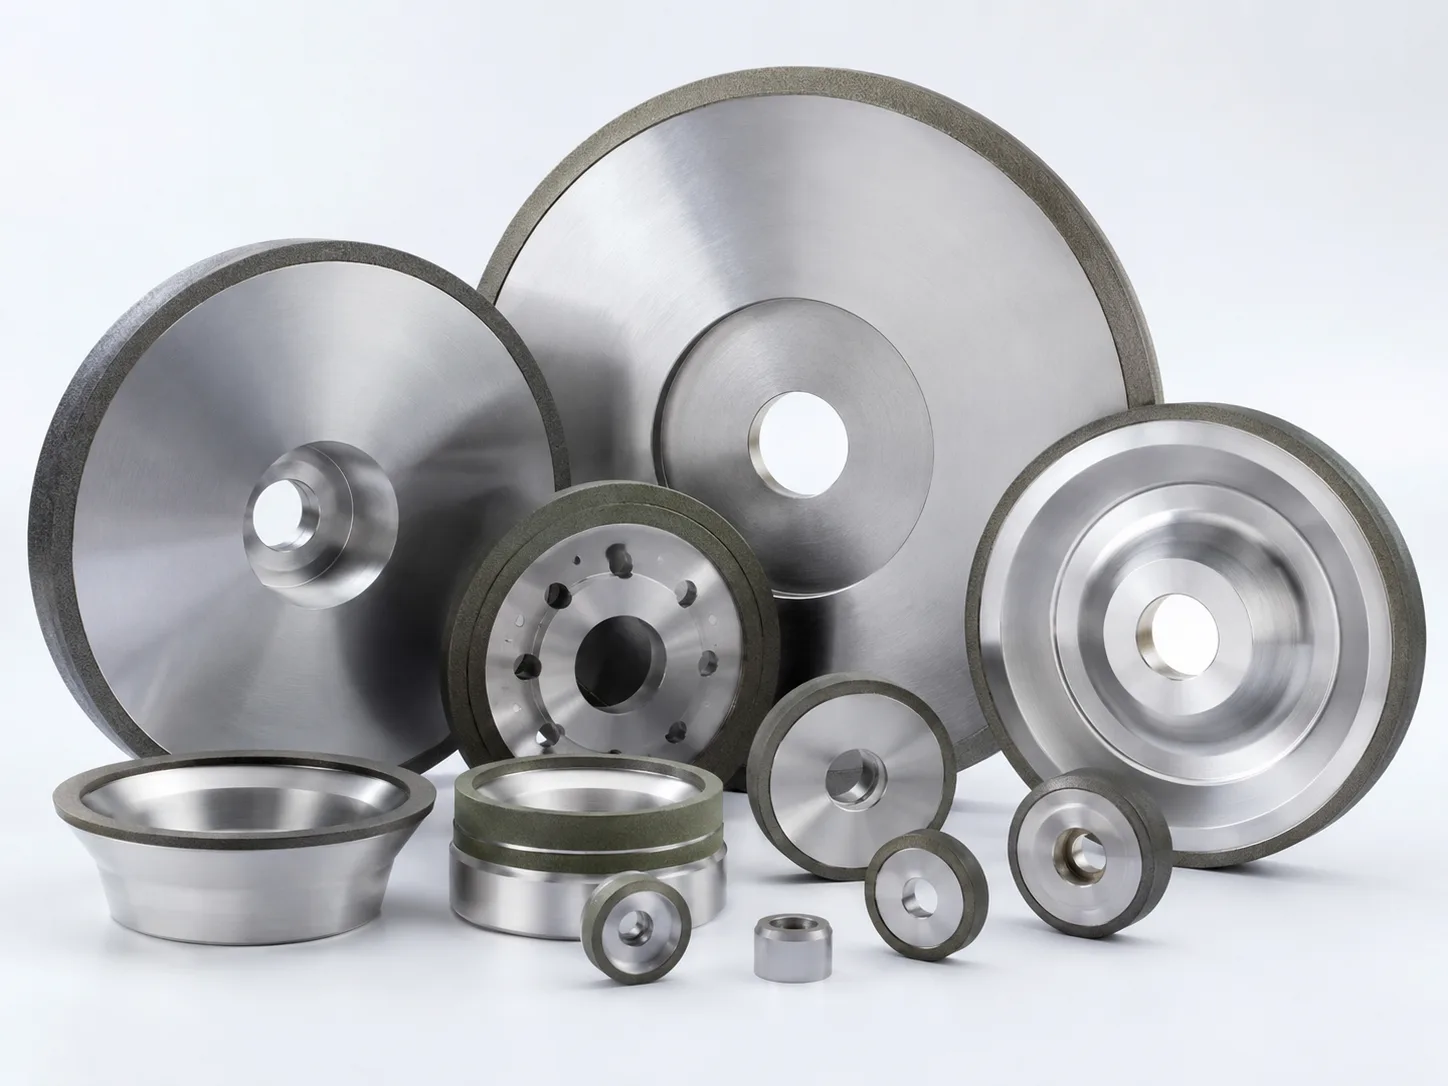
Grinding Wheels for Bearing Grinding Applications: What Buyers Should Review

Grinding Wheel Knowledge Base

Grinding Wheels for Bearing Grinding Applications: What Buyers Should Review

Raceways, bores, outside diameters and end faces create different grinding contacts. Confirm the workpiece condition, wheel details and process evidence before requesting a recommendation.

Mark the raceway, bore, outside diameter or end face on the workpiece drawing
Connect material and hardness with contact area, coolant, dressing and machine condition
Record the current wheel size, profile and full readable specification
Describe where and when burn, chatter, loading, glazing, wear or finish variation appears

Overview

Quick answer

Grinding wheels for bearing grinding applications should be reviewed against the actual workpiece material and hardness, grinding position, contact area, machine, coolant, dressing method, wheel geometry and current problem. A bearing-related wheel name or matching diameter does not establish suitability. Raceway, ID, OD and end-face operations may require different wheel constructions and review directions.

This guide helps buyers prepare bearing grinding application data for review. Youlin supplies grinding wheels, abrasive tools and grinding wheel solutions only. Bearing rings and other bearing components described here are customer workpieces and grinding contexts. Final suitability may require technical review, sample confirmation or a controlled trial.

Start with the exact grinding position

  • An inner-ring raceway and an outer-ring raceway do not create the same access or contact conditions.
  • ID grinding needs bore depth, quill or spindle details and coolant access, not only wheel diameter.
  • Photos help identify visible features, while drawings, measured dimensions and application records provide stronger evidence.
  • CBN may be considered for hardened ferrous materials, but the complete process still determines the review direction.
Conceptual bearing grinding review map showing raceway, inner diameter, outer diameter and end-face contexts
Conceptual application illustration: RACEWAY, ID, OD and END FACE identify different grinding positions. Confirm the real workpiece material, contact and inspection requirements for each operation.

Why bearing grinding needs application review

The useful starting point is the exact surface, material condition and inspection requirement under the real grinding setup.

Separate the bearing context from the wheel decision

A bearing ring identifies the workpiece family, but it does not define abrasive type, grit, grade, bond or structure. Record which ring surface is ground and whether the operation is rough, semi-finish or finish grinding.

Keep requirements measurable

List the applicable drawing requirements and inspection methods for size, roundness, profile, runout or surface finish. Do not replace measured acceptance criteria with a description such as smooth or mirror-like.

Review the complete grinding system

Wheel behavior depends on contact, dressing, coolant delivery, machine rigidity, mounting and process settings. Changing only the wheel may not resolve a symptom caused elsewhere in the setup.

Common bearing grinding situations

Prepare a separate application record when the grinding position, contact or machine setup changes materially.

Raceway grinding

Identify whether the raceway is on an inner or outer ring, then provide the raceway profile, width, contact direction, stock allowance and dressing method. Inner-ring raceway grinding is an external cylindrical context; outer-ring raceway grinding is an internal cylindrical context.

Inner diameter grinding

Provide bore diameter and depth, wheel diameter and width, spindle or quill dimensions, overhang, entry clearance and coolant access. A restricted bore can increase contact, chip-removal and rigidity concerns.

Outer diameter grinding

State whether the operation uses between-centres, chucking, centreless or another setup. Include support, work-rest or fixture details, contact width, traverse or plunge mode and the location of any roundness or chatter problem.

End-face grinding

Identify one-face or double-face grinding, the supported surface, stock distribution and any flatness, parallelism or thickness requirement. Face contact and coolant access differ from cylindrical grinding.

Workpiece material and hardness

Name the material that reaches the wheel

Send the material grade, heat-treatment condition, hardness value and scale, coating if present and the layer being removed. Do not infer the material only from the bearing type or visual appearance.

Record variation within the workpiece

A hardened case, surface treatment or interrupted feature can change the material and contact seen by the wheel. Mark the measurement location and whether the operation crosses into a different layer.

Use hardness as one input

Hardness helps frame abrasive and wheel-grade review, but it does not replace contact area, stock allowance, finish requirement or machine information. Confirm the value rather than using a typical bearing-steel range as if it were measured.

Wheel size, shape, profile and existing specification

Measure the wheel and mounting features

Provide outside diameter, bore, width, recesses, hub or mounting details and available clearance. For small internal wheels, include spindle or quill connection and usable working width.

Document the working profile

A raceway or shoulder may need a formed wheel face. Send a dimensioned drawing of the wheel and workpiece profile, identify the active surface and note where profile loss or edge breakdown occurs.

Preserve the full current marking

Photograph and transcribe every readable element of the existing specification and manufacturer marking. Record unreadable portions as unknown. A similar-looking wheel is not reliable evidence of the same abrasive, bond, grade or structure.

Coolant, dressing and machine condition

Map coolant delivery to the contact zone

State the coolant type, measured concentration when available, filtration condition, nozzle position and whether flow reaches the full raceway, bore or face contact. Record changes across the cycle and visible chip recirculation.

Compare behavior before and after dressing

Provide the dressing method, dresser type and condition, parameters, interval and reason for dressing. Note which profile, finish or grinding symptom returns after dressing and how quickly it changes again.

Include machine and support evidence

Send machine model, wheel and workpiece speeds, feed, infeed, cycle stages, mounting and balance checks. For ID grinding, include quill rigidity and overhang; for OD or raceway grinding, include fixture and support condition.

Conventional, CBN, diamond or custom wheel: what may need comparison

These are review directions, not finished specifications for every bearing grinding application.

Conventional grinding wheels

Aluminum oxide and related conventional abrasive systems may be reviewed for ferrous bearing workpieces. Their suitability depends on material condition, operation, contact, dressing capability and required result. An existing conventional wheel can remain a valid baseline when the controlled process meets the drawing.

CBN grinding wheels

CBN may be considered for hardened ferrous bearing materials. The review still needs bond system, abrasive layer or wheel construction, machine capability, coolant, dressing provision, production condition and inspection evidence. CBN is not automatically required for every ring or raceway.

Diamond grinding wheels

Diamond is generally associated with carbide, ceramics and other compatible non-ferrous or non-metallic materials, and should not be presented as the default for steel bearing grinding because diamond reacts with iron at grinding temperature. Confirm any coating and substrate separately.

Custom wheel construction

A custom bearing grinding wheel may need review when bore access, raceway profile, mounting, coolant clearance or machine envelope prevents a standard configuration. Send drawings and the limiting condition. Feasibility must be confirmed; customization does not mean every requested design can be supplied.

Common mistakes when selecting wheels for bearing grinding

Selecting from bearing name and wheel diameter

The same nominal wheel size can contain different abrasive, grit, grade, bond and structure. Tie the full wheel marking to one documented grinding position and machine setup.

Sending a photo without dimensions or application data

Photos help show a label, profile or visible defect, but perspective cannot confirm dimensions, material hardness or process condition. Add measured wheel dimensions, drawings and operating records.

Changing several variables together

Changing the wheel, coolant, dressing and process settings at the same time makes the result difficult to interpret. Define a baseline and one controlled comparison with agreed inspection criteria.

Evidence for wheel review

Current grinding problem and possible review direction

One visible symptom can have several causes. Record its location and timing before assigning it to the wheel specification.

Conceptual inspection bench with bearing ring, grinding wheel, coolant and drawing for four bearing grinding positions
Conceptual checklist illustration: connect each grinding position with material condition, wheel geometry, coolant access, dressing and machine support.

Raceway grinding

Possible review direction
Review inner- or outer-ring contact, profile generation, wheel-face condition and dressing repeatability.
Information needed
Raceway drawing, ring material and hardness, stock, wheel profile, dressing method and inspection results.

Inner diameter grinding

Possible review direction
Review contact length, wheel-to-bore ratio, quill rigidity, chip clearance and coolant access.
Information needed
Bore diameter/depth, wheel size, quill or spindle details, overhang, cycle and problem location.

Outer diameter grinding

Possible review direction
Review support, work-rest or fixture condition, contact mode, balance and traverse or plunge parameters.
Information needed
Setup drawing, wheel size, support details, speeds, feed and roundness or surface records.

End-face grinding

Possible review direction
Review face contact, stock distribution, support, coolant coverage and wheel-face condition.
Information needed
Face and fixture drawing, stock per face, flatness/parallelism or thickness requirements and measurements.

Burn marks

Possible review direction
Review heat generation, wheel sharpness, coolant delivery, stock and infeed before selecting one cause.
Information needed
Marked defect location, cycle stage, dressing history, coolant evidence and inspection result.

Chatter marks

Possible review direction
Review balance, runout, spindle or quill rigidity, support and vibration together with wheel condition.
Information needed
Mark spacing and location, machine setup, mounting checks, speeds and when chatter begins.

Wheel loading

Possible review direction
Review adhered material, chip space, wheel structure, coolant flushing and dressing effectiveness.
Information needed
Wheel-face photos before/after dressing, workpiece material, time to loading and coolant condition.

Wheel glazing

Possible review direction
Review dull grain exposure, wheel grade, dressing action and the actual grinding load.
Information needed
Wheel-face condition, sound or force changes, dressing record and performance after dressing.

Rapid wheel wear

Possible review direction
Separate wear during grinding from material removed by dressing; review contact and profile demand.
Information needed
Measured size or profile loss, part count or grinding time, dressing removal and failure location.

Unstable finish

Possible review direction
Review dressing consistency, coolant cleanliness, wheel-face change and measurement sequence.
Information needed
Ordered roughness results, measurement method, cycle position and time since dressing.

Application factors to confirm

Use these fields to build one consistent record for each materially different bearing grinding operation. Mark unknown information clearly.

Bearing component type

What to confirm
Inner ring, outer ring or other customer workpiece, plus the exact surface.
Why it matters
The component label alone does not define the contact.
Review note
Mark the grinding position on the drawing.

Workpiece material

What to confirm
Grade, heat treatment, coating and layer being ground.
Why it matters
The contacted material guides abrasive compatibility.
Review note
Do not infer material from appearance.

Workpiece hardness

What to confirm
Measured value, scale and location when known.
Why it matters
Case and core condition may differ.
Review note
State whether grinding crosses layers.

Grinding position

What to confirm
Raceway, ID, OD or end face; rough, semi-finish or finish stage.
Why it matters
Position changes access, contact and profile needs.
Review note
Use a separate record for different setups.

Contact area

What to confirm
Contact width/length, plunge or traverse mode and interrupted features.
Why it matters
Contact affects local load, heat and chip clearance.
Review note
Identify where the symptom concentrates.

Wheel size

What to confirm
Outside diameter, bore, width, recess, hub and clearances.
Why it matters
Mounting and machine-envelope compatibility must be checked.
Review note
Use measured values and a drawing.

Wheel shape/profile

What to confirm
Working face, raceway form, shoulders and mounting geometry.
Why it matters
Profile generation and access depend on geometry.
Review note
Show the active surface and dresser path.

Existing wheel marking

What to confirm
Full readable specification and manufacturer information.
Why it matters
It provides the current comparison baseline.
Review note
Do not guess missing characters.

Coolant condition

What to confirm
Fluid type, measured concentration, filtration, flow and nozzle position.
Why it matters
The contact zone needs cooling and chip removal.
Review note
Confirm access through a bore or across a wide face.

Dressing condition

What to confirm
Method, dresser, parameters, interval and reason.
Why it matters
Dressing changes wheel face and generated profile.
Review note
Compare the same point before and after dressing.

Machine rigidity

What to confirm
Spindle or quill, overhang, mounting, fixture, support and balance.
Why it matters
Deflection or vibration can affect size and finish.
Review note
Record checks from the actual setup.

Current problem

What to confirm
Symptom, location, timing and progression during the cycle.
Why it matters
Sequence helps prioritize review directions.
Review note
Separate observations from assumed causes.

Finish or tolerance target

What to confirm
Drawing requirement, inspection method and current measured result.
Why it matters
Profile, roundness, size and roughness are different outputs.
Review note
Do not substitute visual appearance for measurement.
Conceptual bearing grinding inquiry workflow from application details through technical review to confirmation
Conceptual inquiry workflow: DETAILS → REVIEW → CONFIRM. Confirmation may require more information, a sample or a controlled trial; this illustration does not establish a finished wheel specification.

Buyer checklist

Check the application record before requesting a wheel

A complete record helps identify which technical questions still need confirmation.

1

The exact raceway, bore, outside diameter or end face is marked on the drawing.

2

Workpiece grade, heat treatment, hardness and any coating are stated with unknowns identified.

3

Measured wheel dimensions, mounting, working profile and full readable marking are recorded.

4

Coolant, dressing, machine condition and current problem refer to the same grinding setup.

5

Inspection targets and current results use the same method for a controlled comparison.

Application details

What should buyers send before inquiry?

Prepare one package for each materially different operation. Do not combine raceway, ID, OD and end-face requests without identifying their separate conditions.

  • Workpiece and position

    Bearing application context, inner or outer ring, exact surface, material grade, hardness, heat treatment and coating

  • Wheel and drawing

    Measured wheel size, shape/profile, mounting, full readable specification and dimensioned wheel/workpiece drawings

  • Photos

    Complete wheel, label, working face and marked problem area on the customer workpiece

  • Machine and process

    Machine model, raceway/ID/OD/end-face operation, contact, stock, speeds, feed, infeed and cycle stages

  • Coolant and dressing

    Fluid delivery and condition; dressing method, dresser, parameters, interval and reason

  • Problem and inspection

    Burn, chatter, loading, glazing, wear or unstable finish; location, timing, measured result and drawing target

  • Trial context

    Expected sample or trial quantity, recurring demand if known, baseline condition and information not yet confirmed

Send your bearing grinding application details, wheel size, photos, drawing and current grinding problem. We will review whether the information is enough for a grinding wheel recommendation.

Send Grinding Details →

FAQ

FAQ about grinding wheel review for bearing applications

Questions buyers commonly need to resolve before comparing wheel specifications.

Can one grinding wheel specification cover every bearing grinding operation?

Do not assume so. Raceway, ID, OD and end-face grinding can differ in contact, profile, access, support and inspection requirements. Review each materially different operation before carrying a specification across.

Does bearing grinding automatically require a CBN wheel?

No. CBN may be considered for hardened ferrous bearing materials, while conventional grinding wheels can also be reviewed. The decision depends on material condition, operation, machine capability, coolant, dressing, production context and required result.

Why is diamond not the default for steel bearing grinding?

Diamond reacts with iron at grinding temperature, so it is generally used for compatible non-ferrous or non-metallic materials such as carbide and ceramics. Confirm the actual material and any coating instead of selecting diamond only because it is harder.

What extra information is needed for bearing ID grinding?

Send bore diameter and depth, wheel size, working width, spindle or quill connection, dimensions and overhang, entry clearance, coolant access, dressing method and the exact axial location of size, finish or chatter variation.

Can a wheel be recommended from one photo?

A photo can help identify visible shape, marking or damage, but it cannot reliably establish dimensions, material hardness, contact, machine condition or process settings. Send measured dimensions, drawings and application details as well.

Does an application review confirm final suitability?

An initial review can identify missing information and possible wheel directions. Final suitability may require technical review, sample confirmation or a controlled trial on the actual machine with agreed inspection criteria.